Refurbish or new
Most worn screws can be rebuilt. Here’s when a refurb is the right call, when it’s time for a new screw, and how the job runs.
Refurbishment first
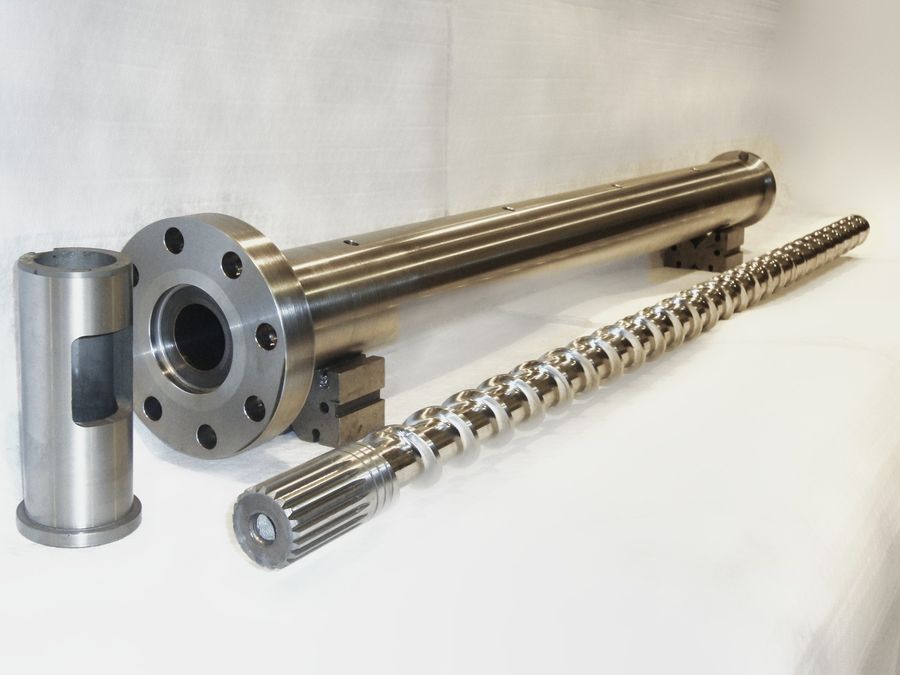
Most extruder screws can be refurbished several times, and a refurb usually costs less than a new screw. Refurbishment typically takes 2–4 weeks.
When to go new
The main limit is root wear. On smaller screws, once the root has worn, a new screw is usually the better option. Root wear affects larger screws less, so they can often be refurbished more times.
A new screw is also the obvious choice if the old one is broken beyond repair, or if you want a spare. New screws typically take 7–9 weeks.
Spares
When we manufacture a new screw, we can refurbish your old one to as-new condition at the same time. That leaves you a spare on the shelf, so the next refurb doesn’t stop the line.
Screw and barrel
If the barrel is worn, we hone it parallel and oversize to remove the wear, then refurbish the screw to suit the new bore. This brings the clearance back to its original standard and is one of the most cost-effective ways to get more life out of the pair. We refurbish barrels from 25 mm to 250 mm diameter and over 6 metres long.
Process
Seized screw?
Our purpose-built 150 tonne press frees screws seized in barrels.
Get in touch
Mon–Thu 07:30–16:15 · Fri 07:30–15:00
Send us the screw, or ask us to measure it once it’s out. Call the workshop or send an enquiry through tws-ltd.com.
Call +44 (0) 1706 655402 Send an enquiry